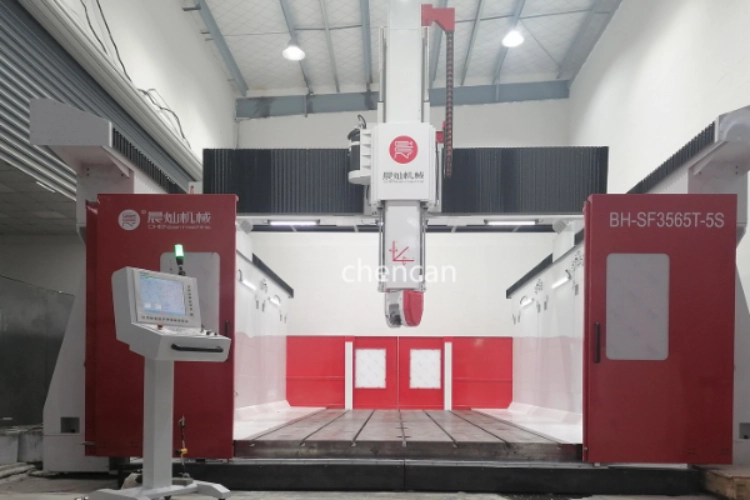
Plan a large CNC machine relocation around a verified receiving site and a documented return-to-production process. Confirm transport access, floor and foundation suitability, utilities, model-specific handling instructions, and acceptance checks before booking the move. CHENcan provides installation and technical support; confirm the relocation scope, service availability, and responsibilities for your particular machine and sites.
Leave a usable record at the old site
Record the model, serial number, controller, options, accessories, and utility requirements alongside the current manuals and drawings. Note alarms, previous repairs, and known accuracy concerns. Where practical, record the machine’s condition and agreed performance checks before shutdown. Photograph connections, cable routes, guards, and leveling points. Back up programs, parameters, offsets, and other supported data using the builder’s procedure; identify the software version and confirm that the backup is readable and suitable for the intended restoration method.
Have the machine builder or a qualified service provider define the permitted disassembly, axis restraints, transport supports, and protection of precision surfaces. Removing an assembly can reduce transport size but add alignment work at installation. Qualified personnel must isolate electrical and other stored energy before disconnection. Professional riggers must use a model-specific lifting plan, verified package weights, approved lifting points, and suitable equipment; photographs are supporting records, not lifting instructions.
Walk the route using the transport dimensions
Survey both sites with the rigging team using the actual transport-package dimensions and weights. Installed catalogue dimensions may omit packing, supports, or removed assemblies. Check doorways, turning space, overhead clearance, ramps, loading areas, and any bridges or lifts along the route. Have the responsible facility or structural specialist assess concentrated loads, equipment loads, and any temporary works before accepting the route.
Continue the survey from the unloading point to the final foundation. Allow space for positioning, assembly, control-cabinet access, maintenance, and peripheral equipment. Verify foundation and anchoring requirements, power, grounding, compressed air, extraction, cooling, and other applicable services against the machine documentation. Give each unfinished site task an owner and deadline, and verify readiness before dispatch.
Define who owns shutdown and backups, disassembly, rigging, packing, freight, unloading, installation, commissioning, and production release. The quotation should separate the service work, travel, transport, and subcontracted activities, with exclusions stated clearly. Assign responsibility for accessory labels, weather protection, any required transport permissions, insurance arrangements, and damage reporting. Confirm support for the actual make and model rather than assuming that every service provider covers every machine.
Check condition while responsibility is still clear
Before packing, inventory accessories and document the machine’s visible condition, including exposed precision surfaces. Repeat the inspection at each agreed transfer of responsibility, particularly after unloading, and record discrepancies in the handover documentation. Agree who receives damage reports, who can authorize repairs, and which records are needed for a transport claim. Retain package labels and condition photographs with the move file.
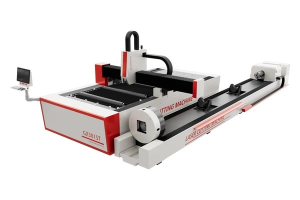
After positioning, follow the builder’s commissioning procedure or an approved plan for the specific machine. Qualified personnel should check connections, transport restraints, leveling, alignment, safety functions, and controlled movement in the required sequence. Geometry, rotary calibration, and compensation checks depend on the machine configuration. Powering up the controller alone does not establish readiness for cutting.
Agree the inspection procedures, calibrated instruments, warm-up requirements, and environmental conditions before taking readings. Compare results with the pre-move baseline and the acceptance limits defined for the machine and intended work. Investigate differences rather than changing compensation simply to obtain a passing reading. Ask the service team to confirm the inspection scope and deliverables; there is no single relocation tolerance suitable for every machine.
Define the last gate back to production
Release the machine only after the agreed safety, commissioning, and performance checks are complete. Use a representative part or production process where required, and inspect the features specified in the acceptance plan. Save readings, program revisions, settings, and authorized compensation changes as the new baseline. Identify who may approve production release and how any open items will be managed.
Build the Schedule Backward from Production Release
Start with the date when production needs a verified machine, then allow time for acceptance testing, commissioning, assembly, positioning, transport, packing, and shutdown. Include any foundation preparation or curing period specified by the responsible specialist. Leave a realistic allowance for inspection findings, replacement parts, or alignment work instead of treating arrival as the production start date.
Use a documented readiness review before dispatch. Confirm the unloading slot, rigging equipment, route approval, receiving crew, foundation status, and utility connection arrangements. Resolve changes to the final machine position before the truck leaves; an alternative location may require a new floor, foundation, and clearance assessment.
Check the packing records from the receiving team’s perspective. Match every loose component, cable, hose, fastener set, and transport restraint to an identifiable label or drawing. State where the backup, manuals, and alignment records are stored. Replace local shorthand with descriptions that an installer unfamiliar with the old site can use.
Keep one controlled move file available to the project owner, rigging team, installer, and receiving production team. Record handover dates, package counts, approvals, and unresolved issues. The commissioning owner needs both the acceptance basis and authority to arrange corrective work; the receiving team needs the same revision of the site and machine information.
Before confirming the truck and crew, complete the relocation planning checklist below.
For equipment and service background, review the CHENcan service page, the CNC machine range, and the company background. To confirm support, site requirements, and a quotation for your specific relocation, contact the service team.
Relocation planning checklist
- Machine records: configuration, condition baseline, manuals, accessory inventory, and a verified backup.
- Handling plan: approved disassembly, lifting, securing, packing, and energy-isolation arrangements for the actual machine.
- Site readiness: transport route, floor capacity, foundation, access space, and required utilities verified.
- Responsibilities: named owners for shutdown, rigging, freight, unloading, installation, commissioning, and release.
- Acceptance: agreed safety, geometry, accuracy, and production checks, with records and sign-off responsibilities.
Approve the acceptance basis before shutdown. A written plan allows the receiving team to assess the reinstalled machine against the same requirements used to prepare the move, with deviations documented and resolved before production release.
Frequently Asked Questions
What records should be completed before a CNC machine relocation?
Keep the machine identity, configuration, manuals, accessory inventory, alarms, repair history, and available pre-move inspection results. Add labeled photographs of connections and components, plus a readable backup created by the builder’s method. Record the software version and restoration requirements so the receiving team can use the data.
Who should approve the disassembly and lifting method?
Follow the machine builder’s model-specific requirements. A qualified service provider should define disassembly and reassembly needs, while the responsible rigging professionals prepare and approve the handling plan. Use verified weights, approved lifting points, suitable equipment, and the required transport restraints.
How should the machine be released back to production?
Complete the machine-specific commissioning and acceptance plan, including the required safety and performance checks. Compare readings with the available baseline and agreed limits, and inspect a representative test part where specified. Keep the results, authorized adjustments, and release approval as the new production baseline.